How to Choose Steel Casing Pipe in 2026?
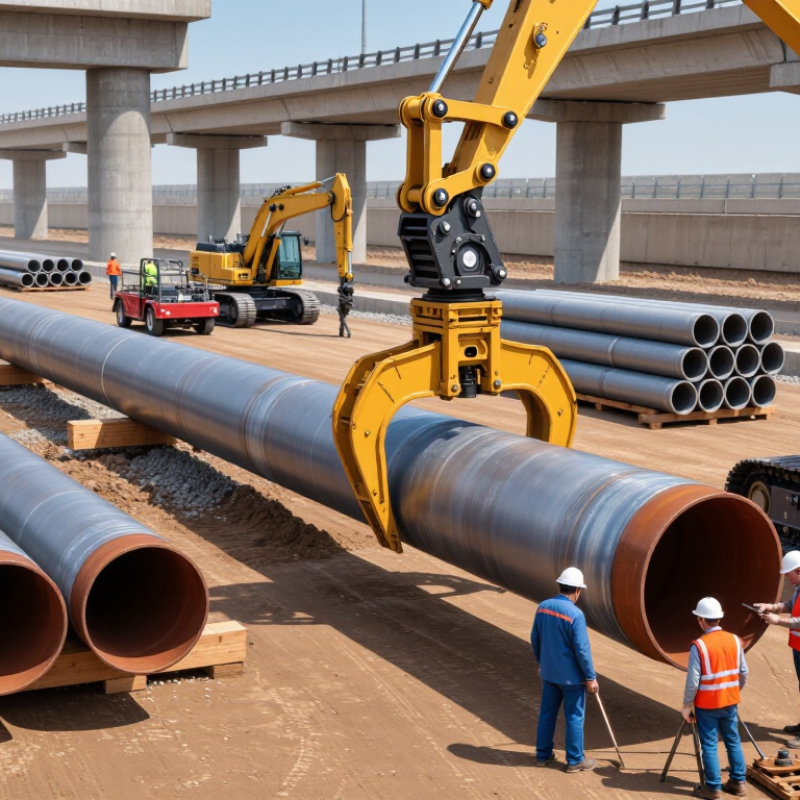
Choosing a Steel Casing Pipe in 2026 requires more than comparing prices, grades, or supplier catalogs. The right selection must match the installation method, soil pressure, groundwater, traffic loads, and carrier pipe dimensions. A casing installed beneath a highway faces different risks from one placed under a railway or river. Small details matter. Wall thickness, outside diameter, steel grade, weld quality, and corrosion allowance can determine long-term performance.
Dr. George A. Antaki, a respected pipeline engineer and author, offers a practical principle: “There is no single best pipe; there is only pipe suited to a specific service.” This idea should guide every purchasing decision. Engineers and contractors should review applicable project specifications, manufacturing standards, end preparation, coating requirements, and inspection records. API 5CT, ASTM A252, and EN standards may be relevant, but no standard should replace project-specific engineering judgment. Certification also deserves careful attention. A familiar logo is not proof of complete suitability.
A useful selection process begins with measured conditions, not assumptions. Confirm the carrier pipe clearance. Calculate external loads. Check whether jacking, boring, open excavation, or another method will be used. Consider handling damage at the site. It happens.
The process is not perfect. Soil data may be incomplete, and future groundwater conditions may change. That uncertainty should be documented, not hidden. A reliable supplier can provide mill certificates, dimensional reports, weld inspection results, and traceable production records. The strongest choice is usually the one that balances structural capacity, installation practicality, service life, and verified evidence. Fancy specifications alone are not enough.
Define Well Loads Using Burst, Collapse, and Tension Design Factors
Match Casing Diameter to Hole Size and Production Needs: API 5CT 4½–20 in
How to Choose Steel Casing Pipe in 2026?
Match Casing Diameter to Hole Size and Production Needs: API 5CT 4½–20 in
Choosing steel casing starts with the drilled hole, not the production target alone. A 9⅝-inch casing does not fit a 9⅝-inch hole. The borehole must provide running clearance, cement space, and room for small deviations. In practice, I check caliper logs before approving the final diameter. A neat drilling plan can still mislead.
API 5CT casing sizes from 4½ to 20 inches cover many oil, gas, geothermal, and water-well designs. Smaller casing may suit limited flow rates and narrow wellbores. Larger casing creates more internal space for tubing, pumps, or higher production volumes. It also demands a larger hole, heavier handling equipment, and stronger surface support. Production forecasts should include pressure changes, sand risk, and future intervention space.
Diameter is only one decision. Select wall thickness and steel grade after reviewing burst, collapse, and tensile loads. Temperature, fluid chemistry, cement density, and connection performance also affect service reliability. Check drift diameter, because nominal size does not equal usable internal space. Centralizers must support the casing without blocking cement movement. I have seen designs fail on clearance assumptions, not pipe strength. That mistake is expensive. Engineers should compare measured hole conditions with API requirements and the actual running procedure. Recheck the design when the well path, mud weight, or completion plan changes.
Select Steel Grade by Yield Strength: J55/K55 55 ksi, N80/L80 80 ksi, P110 110 ksi
How to Choose Steel Casing Pipe in 2026?
Steel grade should match the casing’s required yield strength, not only its purchase price. J55 and K55 provide a minimum yield strength of 55 ksi. They suit moderate loads, controlled depths, and less demanding formations. N80 and L80 reach 80 ksi, offering more resistance when depth, pressure, or handling stress increases. P110 provides 110 ksi for severe loading conditions, but higher strength does not automatically mean better performance.
Start with the load. Review collapse pressure, burst pressure, axial tension, pipe diameter, wall thickness, and connection efficiency. A thicker J55 pipe may outperform a thinner P110 pipe in some designs. That detail is often missed. Temperature, corrosion risk, and fluid chemistry also influence the selection. L80 may require closer attention in sour environments, where material qualification and hardness control become critical. Do not guess.
A reliable specification should identify the applicable casing standard, heat-treatment condition, inspection level, and traceability documents. Request mill test reports and verify yield strength through qualified inspection records. In practical procurement work, mixing grade names with actual mechanical properties creates costly confusion. K55 is not simply a stronger version of J55 in every design decision; manufacturing requirements and application limits matter. One imperfect assumption can affect running performance, connection integrity, and well control margins. Engineers should compare the complete design envelope before approving the pipe.
Choose Connections Under API 5B/5CT for Pressure, Torque, and Seal Integrity
When choosing steel casing pipe in 2026, connection design deserves as much attention as wall thickness. API 5CT defines casing requirements, while API 5B addresses thread dimensions, gauging, and inspection practices. Match the connection to burst, collapse, axial tension, and torque loads. A thread that survives installation may still leak during pressure cycling. That difference matters underground. Review the pressure envelope, temperature range, dogleg severity, and running speed before selecting a connection. Do not treat higher torque as automatic proof of better sealing.
For critical wells, compare connection test data instead of relying on catalog language. Check make-up torque windows, shoulder behavior, metal-to-metal sealing, thread compound compatibility, and galling resistance. Confirm drift diameter after selecting the connection, especially when completion tools must pass. Crews should use calibrated torque-turn equipment and clean, inspected pin and box surfaces. Small debris can change torque response. It is easy to overlook handling damage. Pressure testing should reflect the planned load path, not only a convenient shop test. API compliance supports consistency, but engineering judgment remains necessary.
Tips: Keep connection records by heat, size, grade, and running joint. Verify gauges at required intervals. Use independent inspection when service conditions are severe. If torque data looks unusual, stop and investigate. A rushed make-up can hide a poor seal. Recheck assumptions after the first few joints; real well behavior may challenge the original model.
How to Choose Steel Casing Pipe in 2026?
Choose Connections Under API 5B/5CT for Pressure, Torque, and Seal Integrity
This chart compares common API 5CT casing sizes using nominal outside diameter and representative nominal pipe weight. API 5B covers casing and tubing thread dimensions, gauging, and inspection requirements, while API 5CT defines casing product requirements. Final connection selection should also verify design pressure, make-up torque, seal performance, grade, wall thickness, temperature, and well loads.
Nominal reference values shown: 4½ in × 17 lb/ft, 5½ in × 23 lb/ft, 7 in × 29 lb/ft, 9⅝ in × 47 lb/ft, and 13⅜ in × 72 lb/ft. Connection performance is design-specific and must be confirmed against the applicable API edition and engineering calculations.
Verify Sour-Service Compliance with ISO 15156 and Factory NDT Testing
How to Choose Steel Casing Pipe in 2026?
Sour-service compliance should guide casing selection, not appear as an afterthought. ISO 15156 addresses materials exposed to hydrogen sulfide, especially cracking risks under pressure and tensile stress. It does not certify every pipe automatically. Engineers must confirm chemistry, hardness, strength, and service conditions against the correct material limits.
Factory NDT testing adds practical evidence. Require ultrasonic testing for wall-thickness variations and laminations. Use magnetic-particle or dye-penetrant testing for surface-breaking defects. Review tensile, impact, hardness, and heat-treatment records. Manufacturing traceability matters. Each pipe should connect clearly to its heat number, test report, and inspection results. The IEA Global Methane Tracker 2024 estimated that oil and gas operations released about 120 million tonnes of methane in 2023. Reliable casing integrity supports safer containment, although casing alone cannot prevent every leak.
Tips: Ask for ISO 15156 material justification, not only a compliance statement. Check the NDT method, acceptance criteria, calibration records, and inspector qualifications. Compare factory results with the well’s expected H2S partial pressure, temperature, chloride level, and stress. A polished certificate can still hide weak traceability. I would also inspect sampling frequency carefully; one test per batch may not reflect every pipe. Some specifications remain unclear, and that deserves a written clarification before purchase.
How to Choose Steel Casing Pipe in 2026? - Verify Sour-Service Compliance with ISO 15156 and Factory NDT Testing
Selection checklist for steel casing used in oil and gas wells where hydrogen sulfide (H₂S), pressure, temperature, and manufacturing quality must be evaluated together.
| Evaluation Dimension | What to Verify | Relevant Requirement or Practice | Typical Evidence to Request | Selection Priority |
|---|---|---|---|---|
| Sour-Service Applicability | Confirm whether the planned well environment contains H₂S or could generate sour conditions during production, injection, stimulation, or upset operation. | ISO 15156 addresses materials for oil and gas production in H₂S-containing environments. Applicability should be determined from the actual service conditions, not from the pipe grade name alone. | Approved material-selection basis, H₂S assessment, well-design criteria, and operating-envelope document. | Required |
| ISO 15156 Material Compliance | Check the material, product form, manufacturing route, strength level, heat treatment, and environmental limits against the applicable ISO 15156 requirements. | ISO 15156-1 provides general principles, ISO 15156-2 covers carbon and low-alloy steels, and ISO 15156-3 covers corrosion-resistant alloys. Compliance is condition-specific. | Material compliance statement identifying the applicable part, clause, grade, product form, heat treatment, and environmental limits. | Required |
| H₂S Partial Pressure | Calculate H₂S partial pressure from the gas composition and total absolute pressure at the relevant operating condition. | H₂S partial pressure is a key input in sour-service evaluation. The calculation should use documented gas composition and the most severe credible operating case. | Gas analysis, pressure basis, calculation method, and design-case summary. | Required |
| Temperature and pH | Record minimum, normal, maximum, and transient temperature together with aqueous-phase pH where applicable. | Temperature, acidity, chloride content, water activity, and other environmental variables can affect sulfide stress cracking and hydrogen-related damage susceptibility. | Fluid-property report, corrosion study, operating envelope, and upset-condition assessment. | Required |
| Mechanical Strength | Compare specified minimum yield strength, tensile strength, collapse resistance, burst resistance, and connection performance with the well design loads. | Higher strength does not automatically mean better sour-service performance. The selected material must satisfy both structural design and environmental-resistance requirements. | Certified mechanical test results, design calculations, pipe-body data, and connection qualification records. | Required |
| Hardness Control | Verify hardness measurements for the pipe body, weld area where applicable, heat-affected zones, and connection components. | Hardness limits for carbon and low-alloy steels depend on the applicable ISO 15156 material condition and service environment. Do not use a generic hardness limit without confirming the governing requirement. | Hardness map, test method, test locations, calibration records, and acceptance criteria referenced in the purchase specification. | Required |
| Manufacturing Route | Identify whether the casing is seamless or welded and confirm the specified heat-treatment condition. | Manufacturing route and heat treatment influence microstructure, residual stress, mechanical properties, and resistance to sour-service cracking. | Manufacturing process description, heat-treatment chart, heat number, and traceability records. | Recommended |
| Chemical Composition | Verify carbon, manganese, alloying elements, sulfur, phosphorus, and any additional elements required by the approved material specification. | Low impurity levels and controlled chemistry support consistent mechanical properties and metallurgical performance. Acceptance limits must come from the governing product standard and project specification. | Heat analysis, product analysis where specified, and an original material test report linked to the heat number. | Required |
| Factory NDT: Ultrasonic Testing | Use ultrasonic testing to detect relevant longitudinal, transverse, laminar, or volumetric discontinuities as defined by the inspection specification. | Ultrasonic testing coverage, calibration, scanning pattern, reference standards, and reject criteria must be defined before production. | NDT procedure, equipment calibration record, operator qualification, scan coverage, and individual pipe test results. | Required |
| Factory NDT: Electromagnetic or Magnetic Testing | Apply magnetic particle testing or another approved electromagnetic method where it is suitable for detecting surface and near-surface discontinuities. | The method should match the material, product geometry, discontinuity type, and applicable product standard. It should supplement, not replace, required volumetric testing. | Written procedure, test coverage, sensitivity verification, indications report, and disposition of rejected items. | Conditional |
| Visual and Dimensional Inspection | Inspect outside diameter, wall thickness, length, straightness, ends, threads, coupling fit, surface condition, and marking. | Dimensions and tolerances should follow the applicable casing product specification and purchase order. Thread protection is important during handling and transport. | Dimensional inspection report, thread inspection report, visual inspection record, and photographic evidence where required. | Required |
| Hydrostatic Test | Confirm that each applicable pipe or defined production lot has passed the specified hydrostatic pressure test without unacceptable leakage or pressure loss. | Test pressure, holding time, recording method, and acceptance criteria must be stated in the governing product standard or purchase specification. | Hydrostatic test chart or electronic record, test pressure, hold time, test equipment calibration, and pipe identification. | Required |
| Sulfide Stress Cracking Qualification | Determine whether laboratory qualification or documented service-history evidence is required for the selected material and environmental conditions. | Qualification requirements depend on material category, strength, heat treatment, environment, and the applicable ISO 15156 provisions or project specification. | Test plan, specimen traceability, test conditions, exposure duration, results, and technical review approval. | Conditional |
| Connection Selection | Evaluate connection sealing, galling resistance, make-up torque, tensile efficiency, pressure rating, and compatibility with sour service. | The connection must be assessed as part of the complete casing string. Pipe-body compliance alone does not demonstrate connection performance. | Connection qualification report, make-up procedure, torque-turn record, thread inspection data, and seal-performance documentation. | Required |
| Traceability | Maintain a continuous link between each pipe, heat number, batch, heat treatment, inspection record, and shipping mark. | Traceability should remain intact from raw material through final inspection and delivery. Mixed or incomplete heat numbers should be treated as a quality risk. | Material certificates, heat-treatment records, NDT reports, inspection release note, and packing list cross-reference. | Required |
| Documentation Review | Review certificates before shipment and verify that the documents match the final approved purchase specification. | A complete document package should cover chemistry, mechanical tests, hardness, NDT, hydrostatic testing, dimensions, threads, heat treatment, and nonconformance disposition. | Inspection and test plan, final data book, certificates, NDT summary, calibration certificates, and signed release documentation. | Recommended |
| Nonconformance Control | Check whether any pipe, heat, batch, or connection component has been repaired, reworked, downgraded, or rejected. | Repairs and deviations should be technically reviewed and formally accepted before use. Unapproved rework can change material properties or invalidate qualification. | Nonconformance reports, repair procedures, retest results, concession approvals, and final disposition records. | Required |
| Storage and Handling | Protect pipe ends, threads, coatings, and identification during storage, lifting, transport, and yard handling. | Prevent impact damage, corrosion, contamination, and loss of traceability. Thread protectors and suitable storage supports should be used where required. | Handling procedure, storage inspection checklist, preservation record, and receiving inspection report. | Recommended |
| Final Decision Rule | Select casing only when structural design, sour-service evaluation, manufacturing controls, factory NDT, documentation, and traceability are all acceptable. | ISO 15156 compliance is not a substitute for product inspection, and passing an NDT examination does not by itself prove sour-service suitability. | Signed technical evaluation, approved manufacturer documentation, inspection release, and project acceptance record. | Required |
Note: Acceptance criteria, test frequency, NDT coverage, dimensional tolerances, and material limits should be taken from the applicable product standard, purchase specification, approved inspection and test plan, and the relevant ISO 15156 requirements for the actual service environment.
English
Français